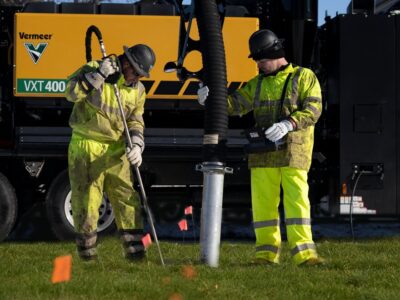
At the end of the day, production is what matters. More potholes completed. More yards of spoil moved. More jobs finished on schedule. When you are shopping for a vacuum truck, the question is not just which one has the best specs. It is which one will help make your crew most productive on the jobs you actually run.
The Vermeer VXT lineup offers three vacuum excavators built for different production demands: the VXT400, VXT500 and VXT600. Each one is engineered around a specific type of work. Here is how to match the right machine to your operation.
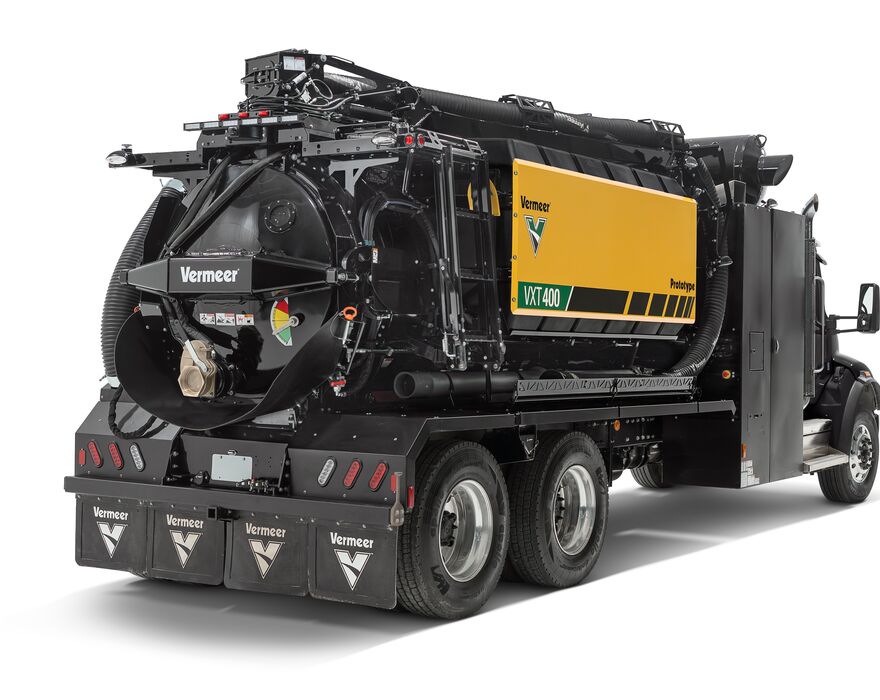
VXT400 vacuum truck: Maximize production in tight spaces
Urban utility work is a game of efficiency. You are hopping between jobsites, navigating narrow streets and working in neighborhoods where a massive truck just slows you down. The VXT400 is built to keep you moving.
With an overall height as low as 11.5 ft (3.5 m), the VXT400 fits under many tree canopies, power lines and low clearances that would force a larger truck to take the long way around. That means less time driving and more time digging.
The side stow boom keeps the dig tube connected during travel, cutting setup time at every stop. The hydraulically driven water system eliminates the unloader valve, removing a common maintenance point that can shut down production mid-job. Reverse flow capability lets you offload drill fluid through the rear gate valve for fast, clean dumping. And with a dry weight starting at 32,500 lb (14,742 kg), you can get more payload on every run, which means fewer trips to the dump site.
Key specs:
- Spoil tank options: 8, 10 or 12 yd³ (6,116, 7,646 or 9,175 L)
- Airflow: 4,131 cfm (117 m³/min)
- Max vacuum: 18 in Hg (0.61 bar)
- Dry weight: Starting at 32,500 lb (14,742 kg)
- Water pump: 3,000 psi (207 bar) at 10 gpm (37.9 L/min), optional 19.4 gpm (73.4 L/min)
- Fresh water capacity: 1,000 to 1,200 gal (3,785 to 4,542 L)
- Boom reach: 16 to 25 ft (4.9 to 7.6 m)
- Boom rotation: 330 degrees
“We built the VXT400 on the same platform as the VXT500 and VXT600,” said TJ Steele, product manager for Vermeer MV Solutions®. “If you have a VXT400 in your fleet and a VXT500 or VXT600, operators can jump from one to the other with minimal training. That flexibility helps keep your crews productive across different job types.”
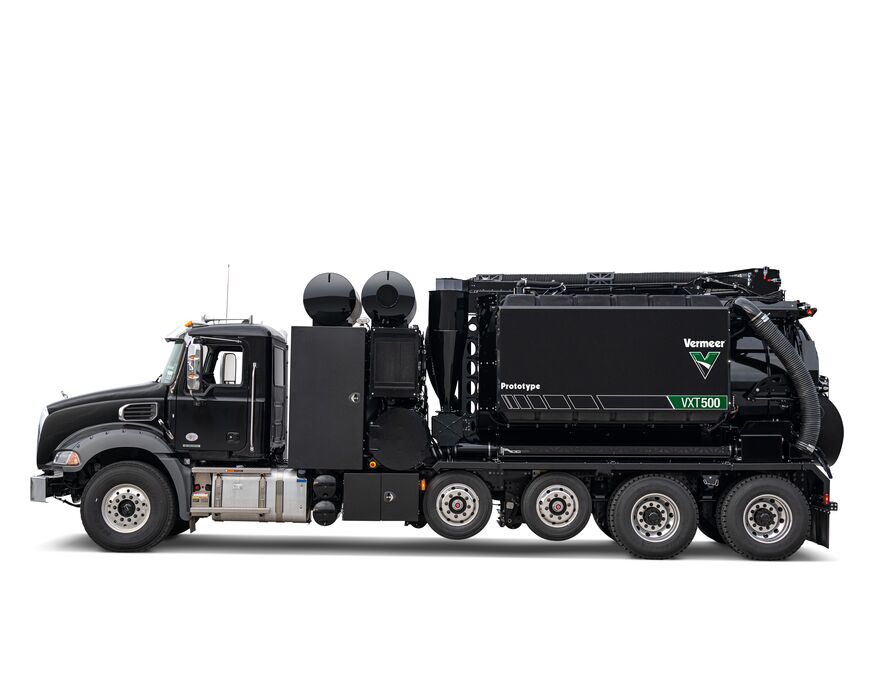
VXT500 vacuum truck: More digging depth, more versatility
Some jobs demand more than standard vacuum power. Deep utility locates. Remote hose work. Drill fluid management on HDD projects. When your production depends on reaching deeper and handling a wider range of applications, the VXT500 delivers.
The key difference is deep vac capability. The VXT500 pulls 27 in Hg (0.91 bar) of vacuum compared to 18 in Hg (0.61 bar) on the VXT400. That extra suction gives you 50% more digging depth, opening up jobs that would otherwise require a larger machine or multiple passes.
The VXT500 also features reverse flow, which lets you offload drill fluid through the rear gate valve for fast, clean dumping. Got a clog in the hose? Reverse the flow and clear it without shutting down. That kind of uptime can add up over a full day of production.
Key specs:
- Spoil tank options: 10 or 12 yd³ (7,646 or 9,175 L)
- Airflow: 5,018 cfm (142 m³/min)
- Max vacuum: 27 in Hg (0.91 bar) deep vac
- Dry weight: Starting at 35,300 lb (16,011 kg)
- Water pump: 3,000 psi (207 bar) at 19.4 gpm (73.4 L/min)
- Fresh water capacity: 1,000 to 1,200 gal (3,785 to 4,542 L)
- Boom reach: 16 to 25 ft (4.9 to 7.6 m)
- Boom rotation: 330 degrees
“The rule of thumb is that with 27 in Hg (0.91 bar), you can theoretically dig up to 27 ft (8.2 m),” Steele explained. “That is a conservative number based on ideal conditions.”
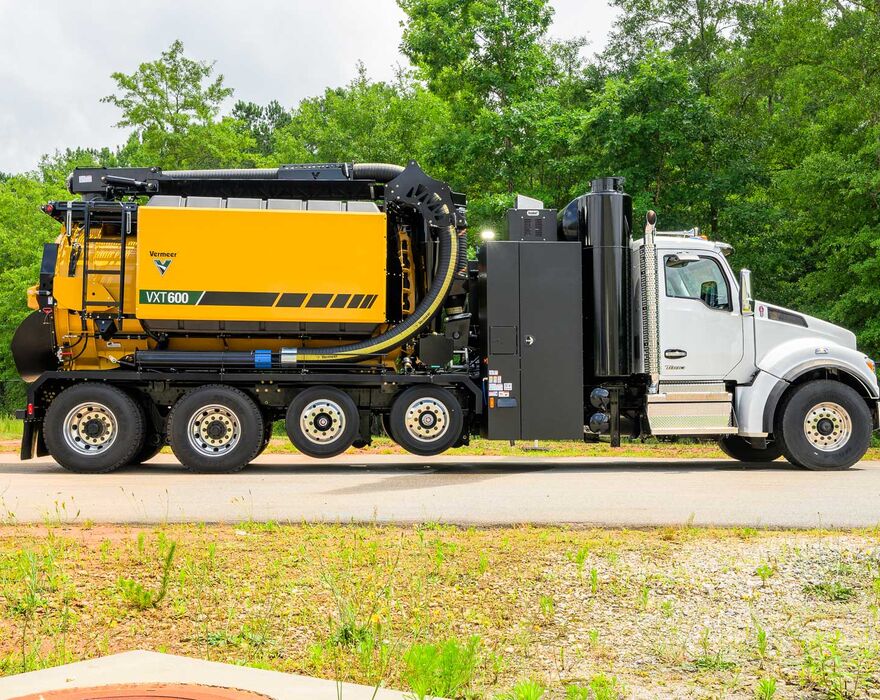
VXT600 vacuum truck: Maximum airflow for high-production work
When production volume is the priority and you need to move material as fast as possible, the VXT600 is built for the job. With a 6,400 cfm (181 m³/min) blower, it delivers the most digging power in the Vermeer vacuum truck lineup.
The VXT600 is engineered for contractors doing long remote hose jobs, specialized excavation work off bridges or any application where raw airflow translates directly into production. At 40,000 lb (18,144 kg), it is also the lightest vacuum excavator in its size class, giving you optimized weight distribution and maximum payload.
One trade-off: the VXT600 does not have reverse flow capability. If offloading drill fluid through the rear gate is critical to your operation, the VXT500 handles that while still delivering serious production. But for contractors who need maximum CFM above all else, the VXT600 is the answer.
Key specs:
- Spoil tank capacity: 12 yd³ (9,175 L)
- Airflow: 6,400 cfm (181 m³/min)
- Max vacuum: 27 in Hg (0.91 bar)
- Dry weight: 40,000 lb (18,144 kg)
- Fresh water capacity: 1,200 gal (4,542 L)
- Overall height: 12.3 ft (3.7 m)
- Boom reach: 25 ft (7.6 m)
Match the vac truck to your production needs
Choosing the right vacuum truck comes down to understanding what drives production on your jobs:
- VXT400: Best for contractors focused on urban utility work where maneuverability and quick setup time drive daily output. Ideal for residential potholing, drill fluid management and jobs where staying on the road with maximum payload matters.
- VXT500: Best for contractors who need deep vac capability and reverse flow to handle a mix of production potholing and mud management. The versatility to take on remote hose jobs without sacrificing efficiency on standard work.
- VXT600: Best for contractors where maximum airflow and spoil capacity drive production. Long remote hose jobs, specialized excavation and high-volume applications where you need the most powerful blower available.
“Most contractors would benefit from having a variety of vac trucks in their fleet for different applications,” Steele noted. “The VXT400 handles your urban and city work where nimble operation drives production. The VXT500 covers production potholing with deep vac capability for those remote hose jobs. And the VXT600 is there when you need maximum CFM to move material fast.”
All three models are built on the latest platform of Vermeer VXT vac trucks, which means operators trained on one can quickly adapt to the others. That flexibility allows fleet managers to move crews between machines as job requirements change, helping keep production consistent across your operation.
For more on making sense of vacuum excavator specifications, check out our guide to understanding CFM, mercury levels and tank sizing.
Once you have the right truck, nozzle selection plays a major role in digging performance. Matching your nozzle size to your water pump output can significantly impact production rates and water efficiency on your job.
Put the right vac truck to work for your operation
The difference between good production and great production can come down to having the right equipment for the work. Your local Vermeer dealer can walk you through the VXT400, VXT500 and VXT600 side by side, talk through your typical job mix and help you spec the vac truck that will drive the most production for your crew. Schedule a demo today and see the difference the right vacuum truck can make.
Vermeer MV Solutions Inc. reserves the right to make changes in engineering, design and specifications; add improvements; or discontinue manufacturing at any time without notice or obligation. Equipment shown is for illustrative purposes only and may display optional accessories or components specific to their global region. Please contact your local Vermeer dealer for more information on machine specifications.
Vermeer, the Vermeer logo, Equipped to Do More and Vermeer MV Solutions are trademarks of Vermeer Manufacturing Company in the U.S. and/or other countries. © 2026 Vermeer Corporation. All Rights Reserved.